Custom Plastic Enclosure Manufacturer – OEM Injection Molding


- group name
- Custom Plastic Enclosure
- Min Order
- 2000 piece
- brand name
- FromRubber Silicone & Plastic OEM Manufacturer
- Nearest port for product export
- FOB shenzhen
- Delivery clauses under the trade mode
- FOB, CFR, CIF, EXW, FCA, DDP, Express Delivery
- Acceptable payment methods
- T/T, D/P D/A, Credit Card, PayPal, Westem Union, Cash
- update time
- Sun, 25 Oct 2026 16:06:19 GMT
Paramtents
Material ABS, PC, PA66+GF, PP, POM
Glass Filled PA66 with glass fiber
Tolerance GB/T 14486 MT3
Surface SPI-A2 to MT-11010 texture
Machine Tonnage 90T to 380T
Structure Snap-fit, bosses, ribs
MOQ 1,000 pcs
Production Mold 14-18 working days
Mold Ownership 100% customer owned
Packing PE bag or export carton
Packging & Delivery
-
Min Order2000 piece
Briefing
Detailed
Custom Plastic Enclosure Manufacturer
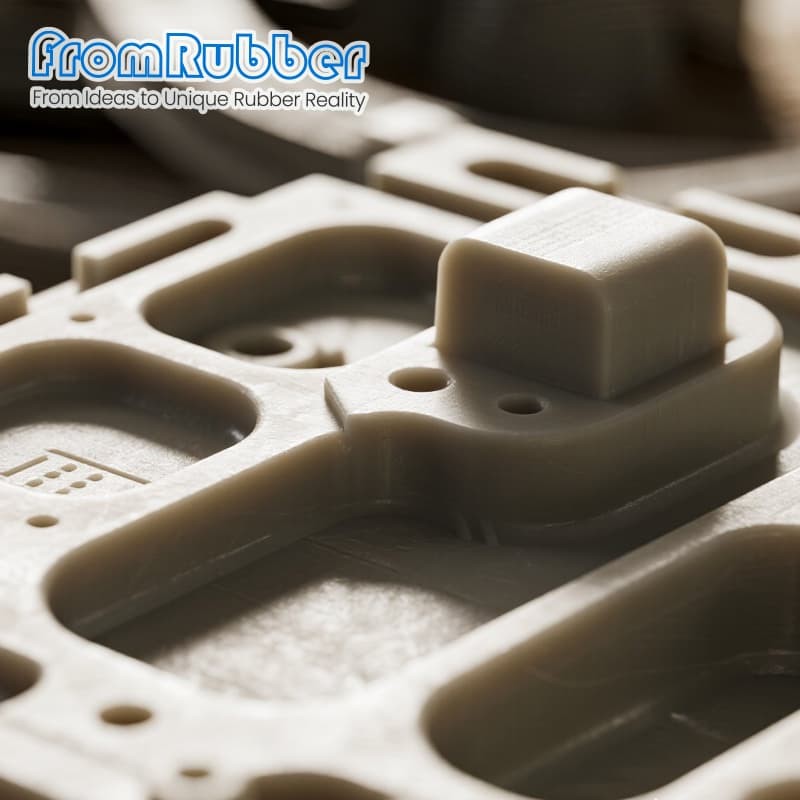
FromRubber injection molds plastic enclosures in ABS, PC, PC+ABS, PA66+GF, PP and POM, from your CAD file or a physical sample. Housings for instruments, junction boxes, power adapters and smart terminals, all from one mold shop. Minimum order is 1,000 pcs per design, and the mold belongs to you once it is paid for.
Structural strength is not a material slogan. It is decided by wall thickness, rib layout, corner radius and where the impact load travels. All four of those live in the mold, which is why we review the load path before we cut steel.
Specifications You Can Set Before Tooling
| Parameter | What you can set |
|---|---|
| Materials | ABS, PC, PC+ABS, PA66+GF, PP, POM |
| Glass-filled option | PA66 with glass fiber for stiffness and heat resistance |
| Tolerance | GB/T 14486 MT3 class |
| Surface roughness | SPI-A2 self-polished down to MT-11010 spark texture |
| Machine tonnage | 90T to 380T, 8 Haitian injection machines |
| Structure | Snap-fit, self-tapping bosses, ribs, ultrasonic weld line |
| Colors | Molded-in color or painted, Pantone matched |
| Surface finish | Texture etching, ink spraying, laser etching, screen printing |
| MOQ | 1,000 pcs per design |
| Production mold | 14-18 working days |
| Bulk delivery | 7-10 working days after order confirmation |
| Mold ownership | 100 percent yours after full payment |
| Mold life | 500,000 to 1,000,000 shots |
How Structural Strength Is Built
Most enclosure failures in the field come from three decisions made at the drawing stage, before material choice even matters. We work through all three in the DFM review and tell you what the shape will and will not survive.
Wall Thickness Stays Even
A sudden step in wall thickness shrinks differently from the section beside it. That leaves a sink mark on the outside and a stress riser on the inside, right where cracks start. We keep the wall even and add stiffness elsewhere.
If a wall must change, the transition gets a taper, not a step.
Ribs Carry the Load
Stiffness comes from ribs, not from a thicker wall. Ribs placed along the impact path absorb the hit and spread it into the shell. Rib depth, thickness and root radius are set against the material shrinkage, or the ribs sink the face they sit behind.
Rib layout is the cheapest strength you can buy.
Corner Radius Sets Failure Point
A sharp external corner concentrates stress and cracks first. A radius turns the impact into a curve that spreads load over a wider area. Where a corner has to stay tight for the product design, we compensate with internal geometry instead.
External radius costs nothing and buys the most.
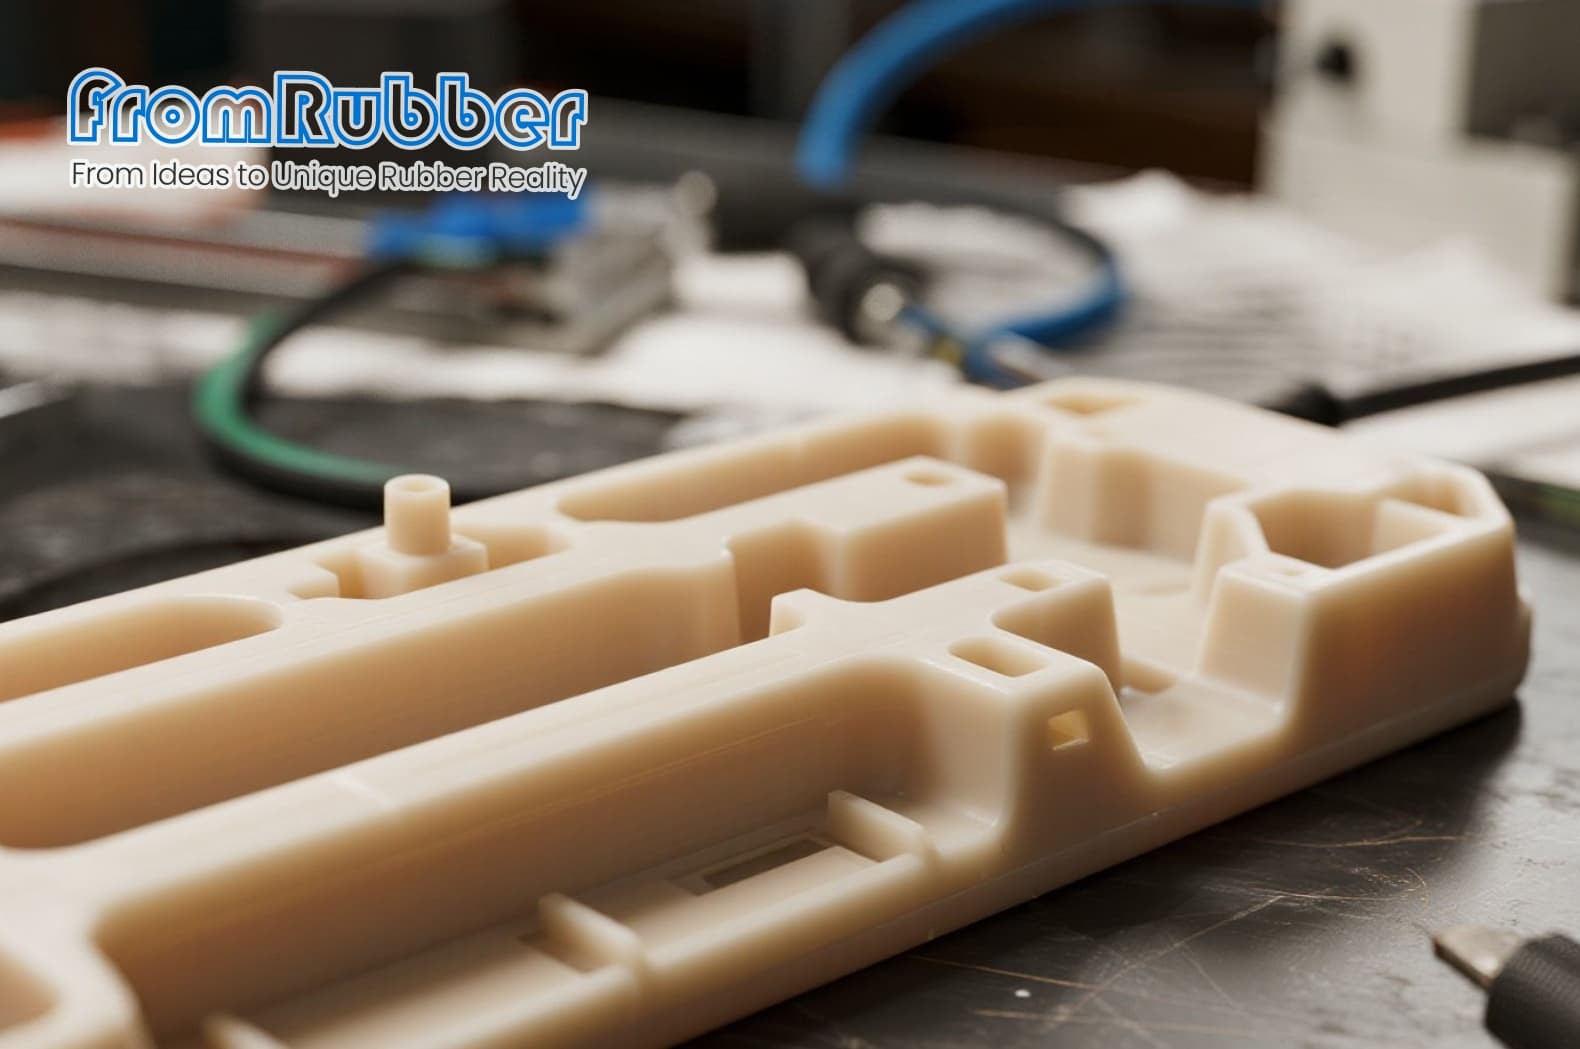
Material comes after geometry. PA66 with glass fiber raises stiffness and heat resistance, which lets a thinner wall do the same job as a thicker unfilled one. That trade has a cost on the surface side, covered in the material table below.
Choosing the Material
| Material | What it gives you | Typical housing | Trade-off |
|---|---|---|---|
| ABS | Clean surface, easy to mold, low cost | General electronics | Moderate chemical resistance |
| PC | Highest impact strength, can be clear | Housings that take hits | Higher cost, needs proper drying |
| PC+ABS | Balance of the two above | Most electronic enclosures | Neither extreme |
| PA66+GF | High stiffness, heat resistance, stable dimensions | Structural and load-bearing parts | Narrower texture range, tool wear |
| PP | Chemical resistance, light weight | Chemical and hinged parts | Low stiffness |
| POM | Wear resistance, self-lubricating | Sliding and moving parts | Hard to bond |
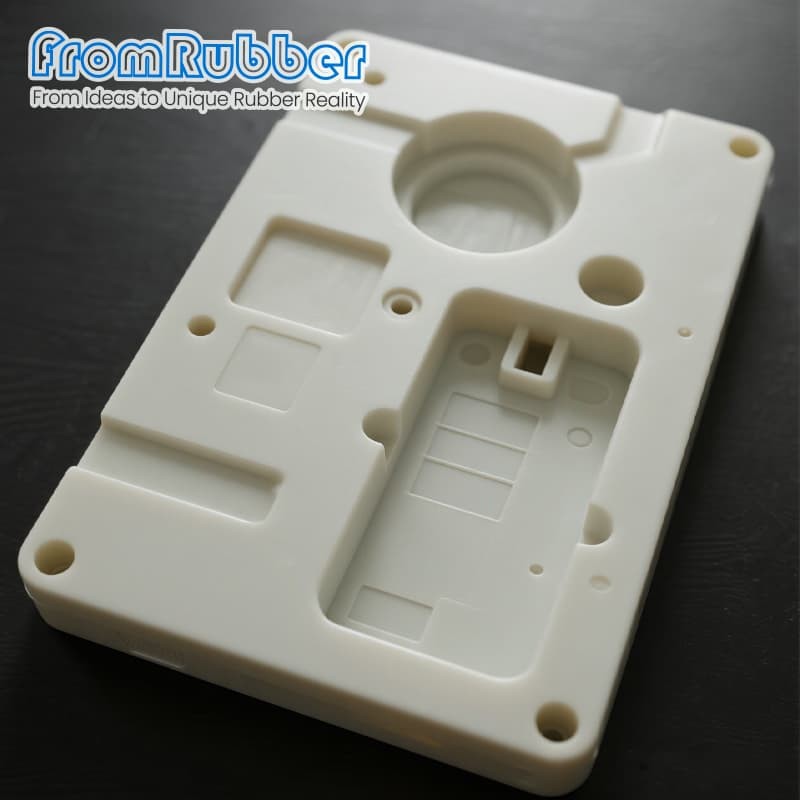
Which material fits your housing? If the part is mostly a shell with light loads, ABS or PC+ABS keeps cost down and gives the best surface. If it carries a PCB, a battery pack or a mounting bracket, PA66+GF holds shape under load and heat.
Send the drawing and tell us where the impact lands and what the part has to carry. We will name the material and the wall thickness together, because changing one changes the other.
Structure Features We Mold
Snap-Fit Joints
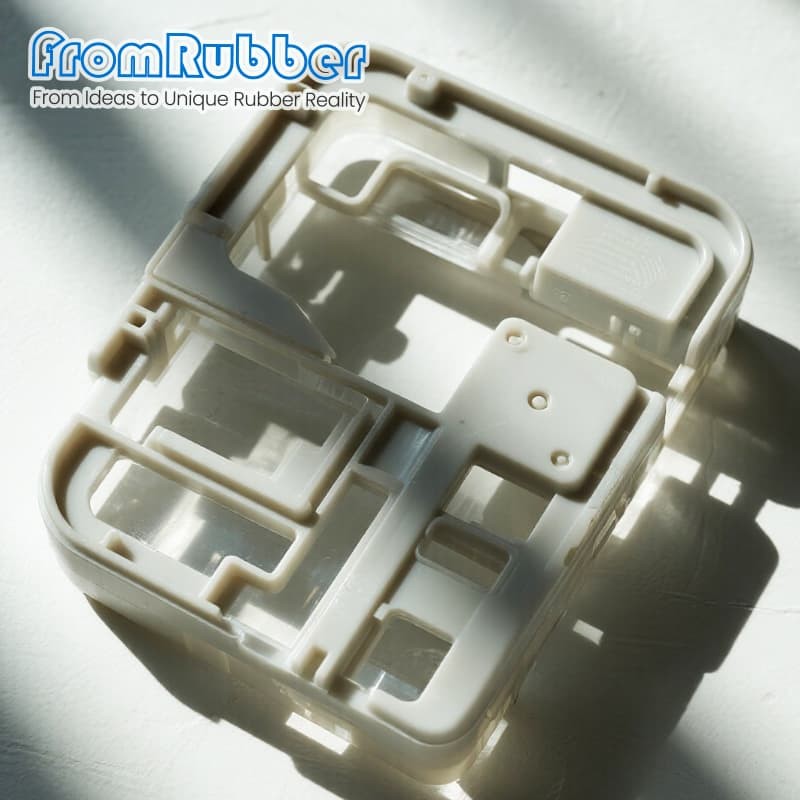
Living hinges and cantilever snaps molded in the same shot, so the two halves assemble without screws. Undercuts are designed where the mold can release them.
Self-Tapping Bosses
Boss diameter, wall thickness and pilot hole are sized to the screw and the material, so the boss does not split on first assembly.
Reinforcing Ribs
Rib depth, thickness and root radius matched to shrinkage, so stiffness goes up without sink marks appearing on the visible face.
Ultrasonic Weld Lines
Energy director geometry molded into the joint, so the two halves weld into one sealed body without adhesive.
Surface Finishes
- Texture etching from SPI-A2 self-polished mirror down to MT-11010 spark texture. Leather-grain patterns can be etched into the tool.
- Ink spraying for full matte, soft-touch or anti-scratch surfaces, with film thickness held at 10-25 micrometre.
- Laser etching with a 0.015 mm spot to cut through coating and expose the base for markings.
- Screen printing with registration held to plus or minus 0.05 mm for labels, scales and logos.
- Molded-in color when the part must not show scratches, since the color runs through the wall.
Glass-filled nylon and high-gloss finishes pull against each other. Fiber shows through a mirror polish, so a PA66+GF part usually lands on a matte or textured surface. If your product needs both stiffness and gloss, we will suggest splitting the part instead of compromising both.
How an Order Runs
| Step | What happens | Timing |
|---|---|---|
| 1 | You send CAD or a sample. We review wall thickness, ribs and draft, then quote. | 3 hours for a clear drawing |
| 2 | Mold design is confirmed with you before any steel is cut. | By written approval |
| 3 | Production mold is built and trialed. | 14-18 working days |
| 4 | First article inspection against your drawing, then your sign-off. | Before mass run |
| 5 | Mass production with in-line inspection and final inspection. | Scheduled after order |
| 6 | Bulk goods delivered. | 7-10 working days after order confirmation |
The injection molding line runs on 8 Haitian machines from 90T to 380T. If your schedule is tight, the quick proofing service shortens the front end of the project.
What We Need From You
- 3D file in STEP or IGES, or a 2D drawing in DWG, DXF or PDF. A physical sample also works, we reverse-engineer the geometry from it.
- Material and color, or the environment the part has to survive.
- Surface finish: texture, matte, gloss, or molded-in color.
- Assembly requirements: PCB size, screw type, mating part.
- First order quantity and estimated annual usage.
Where These Housings Go
Handheld Instruments
Field test meters and portable analyzers that get set down hard, dropped and knocked against equipment. The shell has to absorb that and still hold the display flat.
Industrial Control Boxes
Junction boxes and control housings mounted on machines, where vibration is constant and the cover has to stay sealed.
Medical Monitor Housings
Bedside monitors and diagnostic units where the surface must clean easily and the shell protects the electronics inside.
Smart Home Terminals
Wall-mounted and desktop terminals where appearance matters as much as the fit, and the housing is part of the product identity.
Power Adapter Enclosures
Charger and adapter shells where the wall has to clear internal components and still pass the drop and heat requirements of the destination market.
Dashboard and Vehicle Housings
In-cabin electronic housings that face temperature swings, vibration and UV, and have to match the interior finish around them.
The Factory Behind the Enclosure
| Staff | 220 |
| Workshop | 12,000 sqm and above |
| Injection machines | 8 Haitian, 90T to 380T |
| In-house mold shop | 7 CNC machines plus EDM |
| Molds in storage | 7,254 sets |
| Custom projects delivered | 6,532 |
| First-pass yield | 92 percent |
| Certification | IATF 16949:2016, ISO 9001:2015, ISO 14001:2015 |
Frequently Asked Questions
Can you mold from a physical sample instead of a CAD file?
Yes. Send the sample and we reverse-engineer the geometry. This is common when the original drawing was lost or when the part to copy is a competitor product.
What is the minimum order?
1,000 pcs per design. The floor exists because the mold and the machine setup cost the same whether you run 1,000 or 100,000.
My housing failed a drop test. Can you fix the structure?
Usually yes, and it is cheaper to fix in the drawing than in the field. Send the failed part and tell us where it cracked. Cracks almost always start at a sharp corner, a wall step, or a rib that sank the face it sat behind, and all three are mold-side decisions.
Does glass-filled nylon limit the surface finish?
Yes. Fiber shows through a high polish, so PA66+GF parts normally take a matte or textured finish. If you need a mirror surface and high stiffness together, split the part so the visible shell and the structural frame use different materials.
How long does the mold take?
14-18 working days for a plastic injection mold, measured from design approval. Bulk delivery is 7-10 working days after order confirmation.
What can you not make?
Parts that exceed our 380T machine capacity, and specialty engineering plastics outside our regular material list. We will tell you before quoting rather than after.
What kinds of enclosures do you mold?
Instrument housings, junction and control boxes, power adapter shells, medical monitor housings, smart home terminals and vehicle dash housings. Anything that fits within a 90T to 380T machine and our material list, we can quote.
How fast is the quotation?
3 hours for a single part with a clear drawing. Complex multi-part assemblies take up to 24 hours.
Send the Drawing. We'll Tell You Where It Cracks First.
- Send a STEP or IGES file, a 2D drawing, or a physical sample
- Get the quotation plus the weak points we found, within 3 hours
- Free DFM review on wall thickness, rib layout and corner radius before tooling
- The mold is yours, and an NDA is available on request
The inquiry form accepts .zip, .rar, .pdf, .jpg, .png, .doc and .xls up to 20 MB. Put STEP or DWG files inside a .zip.